The global textile landscape is witnessing a significant shift toward versatile blended materials that balance comfort, durability, and cost-effectiveness. Among these, the development and application of fabrics like the cotton polyester lycra fabric concept represent a drive toward creating garments that adapt to the wearer's movements while maintaining a professional appearance. Understanding these blends is crucial for manufacturers seeking to optimize production costs without compromising on the quality expected by modern consumers.
In the competitive world of garment manufacturing, the demand for fabrics that resist wrinkling yet remain breathable has led to the proliferation of technical blends. While traditional poplin is celebrated for its classic utility, the industry often looks toward cotton polyester lycra fabric characteristics to solve issues related to fabric recovery and shape retention. This evolution reflects a broader industry trend where synthetic fibers are strategically integrated with natural cotton to enhance the longevity of everyday apparel.
For procurement managers and fashion designers, selecting the right material involves a delicate balance of weight, composition, and finish. Whether it is the economical nature of TC poplin or the stretch capabilities of a cotton polyester lycra fabric, the goal remains the same: providing high-performance textiles that meet rigorous international standards for color fastness and fiber strength.
Global Relevance of Blended Textiles
The global textile market is increasingly reliant on blended fabrics to meet the diverse needs of different climates and economic zones. In regions like Africa, South-East Asia, and the Middle East, there is a high demand for materials that are durable, easy to maintain, and affordable. Blends that incorporate polyester provide the necessary strength and light resistance, while cotton ensures the comfort and breathability required for hot and humid environments.
This global shift is supported by ISO standards that emphasize the need for consistency in fiber strength and color fastness. By optimizing the ratio of natural to synthetic fibers, manufacturers can produce fabrics that withstand rigorous daily use—such as in uniforms or workwear—while reducing the overall cost of production. This makes high-quality apparel accessible to a wider population, bridging the gap between luxury textiles and economical utility.
Defining the Hybrid Composition
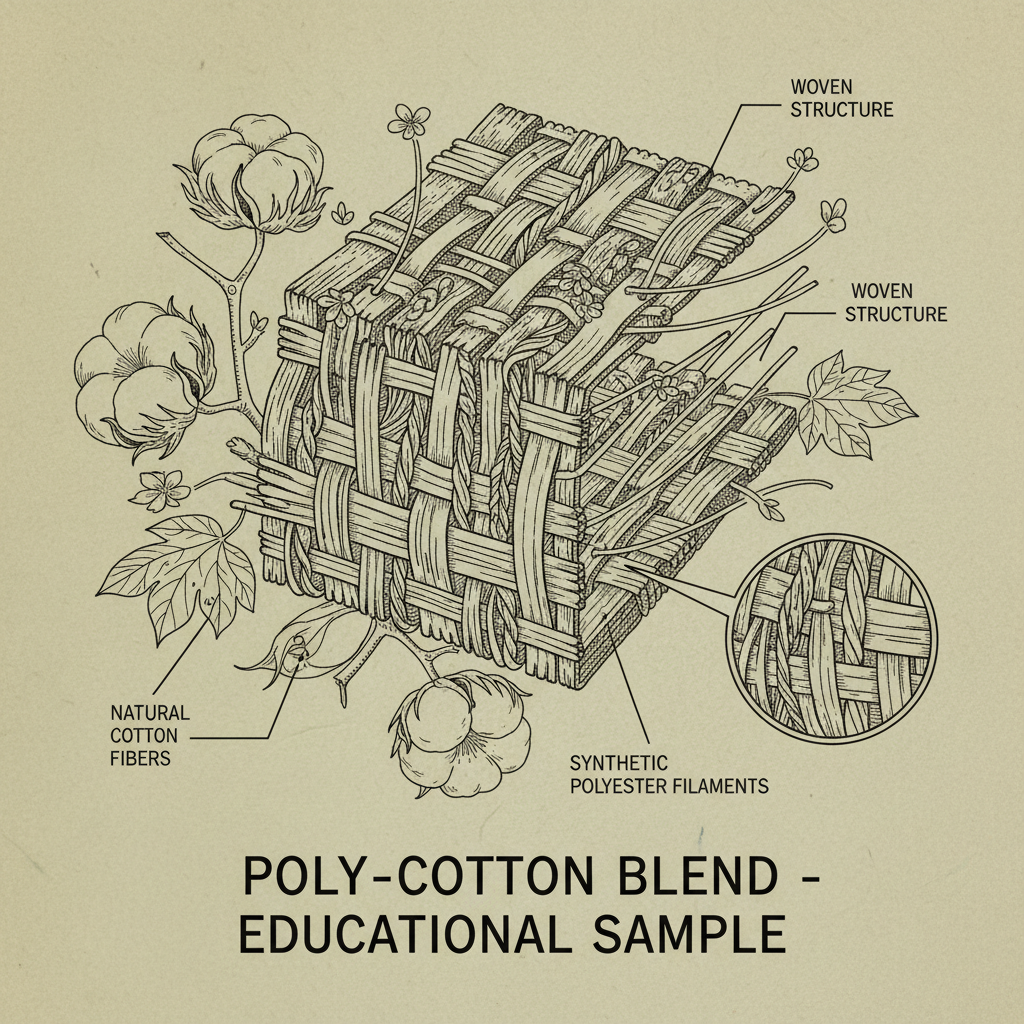
At its core, a hybrid composition like cotton polyester lycra fabric is designed to synthesize the best properties of three distinct materials. Cotton provides the soft hand-feel and moisture absorption, polyester contributes high fiber strength and resistance to folding, and lycra adds the essential elasticity that allows the fabric to stretch and return to its original shape.
In the context of professional apparel, such as shirts or medical scrubs, this composition solves the problem of "bagging" at the elbows or knees. Unlike 100% cotton, which may lose its shape over time, or 100% polyester, which can feel stifling against the skin, the blended approach ensures a garment remains crisp and comfortable throughout a long workday.
From a manufacturing perspective, these blends are often processed using continuous dyeing techniques and mercerization to achieve a neat, bright surface. This ensures that the final product not only performs well mechanically but also meets the aesthetic requirements of the global fashion and corporate wear markets.
Core Components of Performance Fabrics
The durability of a cotton polyester lycra fabric is primarily derived from the polyester component. Polyester is known for its incredible tensile strength and resistance to abrasion, which ensures that the fabric does not wear through easily, even in high-friction areas. This makes it an ideal choice for industrial aprons and pocketing fabrics where longevity is a non-negotiable requirement.
Cost efficiency is another pillar of these blends. By utilizing a percentage of polyester—such as in the 65% polyester and 35% cotton TC poplin—manufacturers can significantly lower the cost compared to pure cotton textiles. When the elasticity of cotton polyester lycra fabric is added, it adds a premium functional value that justifies the price point for end-users who prioritize fit and mobility.
Finally, the comfort and breathability provided by the cotton element are essential for skin-contact garments. Cotton allows air to circulate and absorbs moisture, preventing the "plastic" feel often associated with high-synthetic fabrics. This synergy ensures that the cotton polyester lycra fabric remains a top choice for a wide variety of applications, from casual shirts to specialized workwear.
Practical Industrial Applications
The application of these blended textiles spans across various sectors, from the hospitality industry to healthcare. In the production of corporate shirts and aprons, the balance of strength and softness is key. Many manufacturers leverage the air-jet quality of poplin and the flexibility of cotton polyester lycra fabric to create garments that look professional but feel like athletic wear.
Furthermore, in remote industrial zones or post-disaster relief operations, there is a critical need for lightweight yet sturdy fabrics for temporary clothing and gear. Fabrics with a weight between 70 gsm and 175 gsm provide the necessary protection without adding excessive bulk, ensuring that workers and volunteers can move freely and efficiently in challenging environments.
Performance Metrics for Different Blends
Long-Term Value and Reliability
The long-term value of investing in a high-quality cotton polyester lycra fabric lies in its reduced replacement cycle. Because these fabrics are engineered for heat resistance and light resistance, they do not fade or degrade as quickly as pure natural fibers when exposed to sunlight or industrial washing processes. This reliability is a critical factor for companies providing uniforms to thousands of employees.
Moreover, the emotional value of "dignity in dress" is enhanced when a garment maintains its shape and color over time. A shirt that doesn't wrinkle excessively and fits the body comfortably boosts the wearer's confidence. By combining the softness of cotton with the resilience of synthetics, manufacturers provide a product that balances logical cost-saving with the psychological need for professional presentation.
Future Innovations in Fiber Blending
The future of the cotton polyester lycra fabric sector is leaning heavily toward sustainability. We are seeing a rise in the use of recycled polyester (rPET) and organic cotton, which reduces the environmental footprint of the textile industry without sacrificing the fabric's physical properties. Digital transformation in the dyeing process is also reducing water waste, making the production of TC fabrics more eco-friendly.
Automation in air-jet weaving is allowing for even tighter control over density and yarn count, resulting in fabrics that are thinner yet stronger. This allows for the creation of "ultra-light" poplins that still possess the durability required for industrial use, further expanding the versatility of blended textiles.
Additionally, smart textiles are beginning to integrate conductive fibers into these blends. Imagine a cotton polyester lycra fabric that can monitor heart rate or body temperature—the stability of the polyester and the stretch of the lycra provide the perfect substrate for embedding electronic sensors without compromising wearer comfort.
Overcoming Manufacturing Challenges
One of the primary challenges in producing a cotton polyester lycra fabric is ensuring consistent color fastness across different fiber types. Polyester and cotton react differently to dyes, which can lead to "frosting" or uneven tones. To solve this, professional manufacturers use continuous dyeing techniques and a rigorous grading system, ensuring that light and middle colors reach a grade 4 fastness, while dark colors maintain a steady grade 3.
Another hurdle is the control of shrinkage. The introduction of lycra can make the fabric prone to instability if not properly heat-set. Expert knowledge—often built over decades, such as 35+ years of experience—is required to calibrate the tension and temperature during the finishing process to ensure the fabric remains straight and stable after multiple washes.
Lastly, balancing the "hand-feel" while maintaining high fiber strength requires precise mercerization. This chemical treatment increases the luster of the cotton fibers and improves dye affinity, resulting in a fabric that feels soft to the touch but remains rugged enough for heavy-duty application.
Technical Analysis of Fabric Composition and Performance
| Composition Type |
Elasticity Score (1-10) |
Durability Rating |
Primary Use Case |
| TC Poplin (65/35) |
4 |
High |
Corporate Shirts |
| Cotton Poly Lycra |
10 |
Medium-High |
Stretch Workwear |
| 100% Cotton Poplin |
2 |
Medium |
Eco-Casual Wear |
| 100% Polyester |
3 |
Very High |
Industrial Aprons |
| CVC Blended Fabric |
5 |
High |
Premium Uniforms |
| Poly-Cotton-Satin |
6 |
Medium |
Hospitality Linens |
FAQS
The main advantages include significantly higher durability, better resistance to wrinkling, and enhanced shape retention. While 100% cotton is breathable, it tends to shrink and crease easily. The addition of polyester and lycra ensures the garment maintains its professional appearance throughout the day and withstands more wash cycles without losing its fit.
Yes, blends incorporating polyester generally offer better heat resistance and fiber strength than pure natural fibers. However, it is important to check the specific GSM and composition; for instance, our TC poplin is engineered for durability and light resistance, making it suitable for various industrial applications including aprons and protective clothing.
Air-jet weaving is a high-efficiency process that results in a more uniform and denser fabric surface compared to traditional weaving. This leads to a smoother finish, better structural integrity, and a more consistent feel, which is essential for high-end shirts and precise garment construction.
Absolutely. Depending on whether you prioritize softness (more cotton), durability (more polyester), or stretch (more lycra), the ratios can be adjusted. We offer various compositions including 100% cotton, 100% polyester, and tailored poly-cotton blends to meet specific regional or functional requirements.
For high-quality blends, we typically achieve a color fastness grade of 4 for light and middle colors, and grade 3 for darker tones. This is achieved through professional continuous dyeing and mercerization, ensuring the colors remain vibrant even after repeated exposure to light and washing.
The weight of the fabric is measured in GSM (grams per square meter). For lightweight shirts, a range of 70 gsm to 110 gsm is ideal. For more rugged applications like pockets or aprons, a weight closer to 175 gsm is recommended. Always reference the technical data sheet for the specific GSM of the batch.
Conclusion
The integration of natural and synthetic fibers, exemplified by the cotton polyester lycra fabric approach, represents the pinnacle of practical textile engineering. By combining the breathability of cotton, the strength of polyester, and the flexibility of lycra, manufacturers can produce high-performance textiles that meet the rigorous demands of the global market while remaining economically viable.
As the industry moves toward more sustainable practices and smart-textile integration, these blended fabrics will continue to evolve, offering even greater efficiency and environmental responsibility. For those seeking a partner with over 35 years of expertise in poplin and blended textiles, we invite you to explore our capacity for high-volume, fast-delivery solutions. Visit our website: www.bosswintextile.com